Features
Everything between your drawing and the machine
NativeCAM covers the whole CAM step for a CNC router: import or draw the design, choose bits, make toolpaths, simulate them and export a checked file for your controller.
Design import
Draw rectangles, circles, ellipses, polygons, stars and text in any installed macOS font, or bring artwork in with ⌘I or by dropping files on the canvas.
- DXF: lines, arcs, circles, polylines with bulges, splines, ellipses, blocks and inserts, and
$INSUNITS. POINT entities become drill marks, and loose segments are chained into closed loops. - SVG: the full path grammar, transforms and viewBox units.
- PDF and Illustrator
.ai(PDF-compatible): nested groups, page rotation and the crop box. Clipping masks trim what they cover and hidden layers are left out, as a PDF viewer shows them. - 3D meshes: STL (binary or ASCII), OBJ, 3MF (including Bambu and Prusa multi-part files), USDZ/USD and PLY. Choose the up axis, flip, size, carve depth and how far below the surface the top sits.
Toolpaths
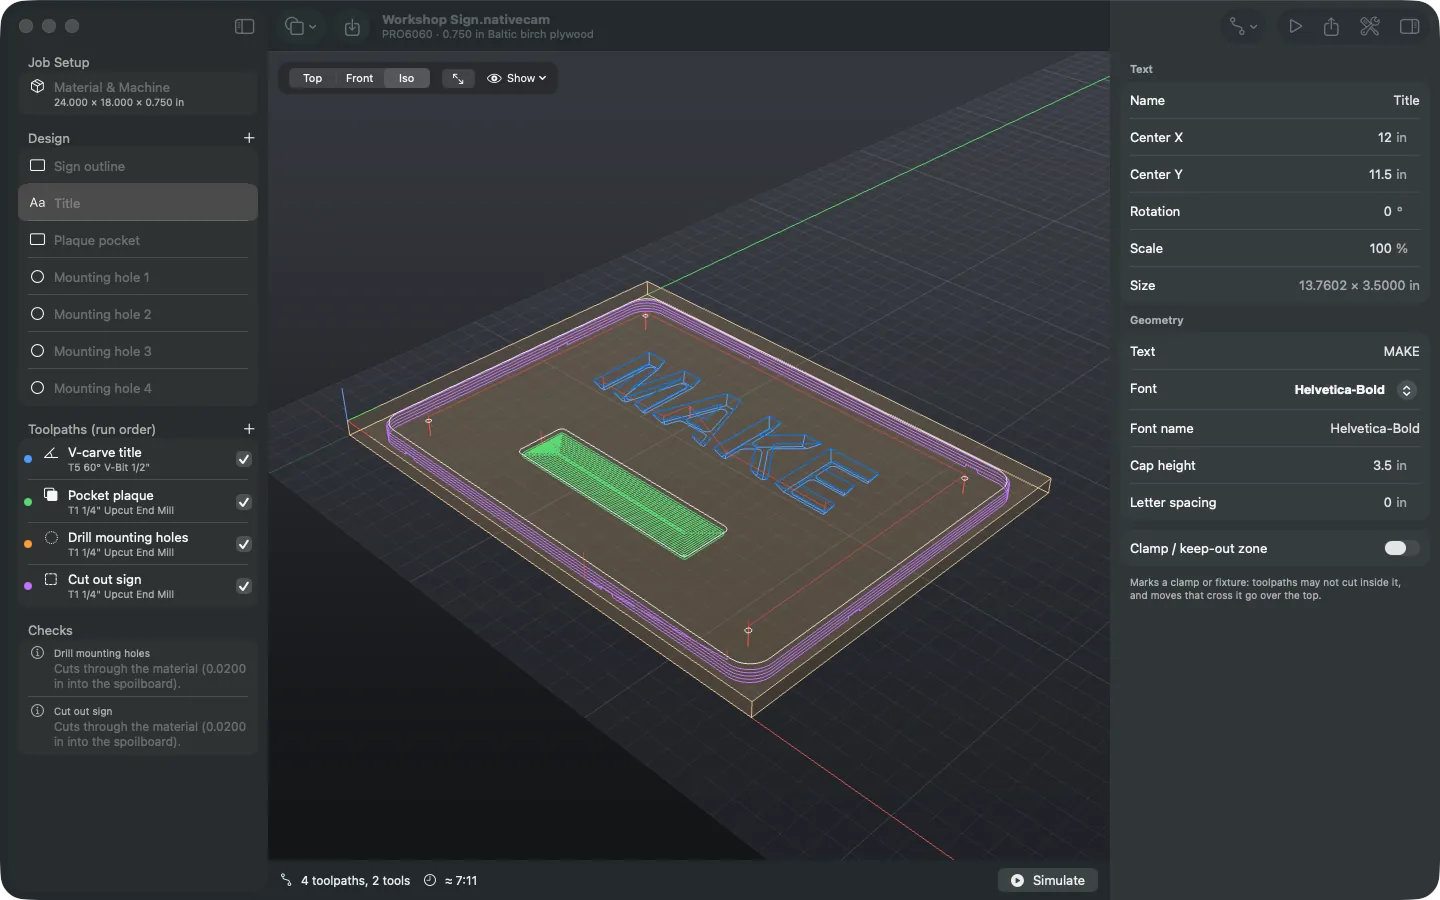
Select vectors, then add a toolpath from the toolbar or by right-clicking them. Toolpaths run in sidebar order: drag to reorder, or choose Toolpaths ▸ Optimize Run Order for the fewest tool changes that still cuts the inside of each part before its cut-out.
| Toolpath | What it does |
|---|---|
| Profile | Inside, outside or on the line; climb or conventional; multi-pass; ramp entry; arc or line leads in and out; dogbone or T-bone corners; tabs; allowance. Holes are cut before outside profiles. |
| Offset or raster clearing, islands, safe feed links between regions, dogbone or T-bone corners. Inner clearing rings get rounded corners while the wall pass stays exact. | |
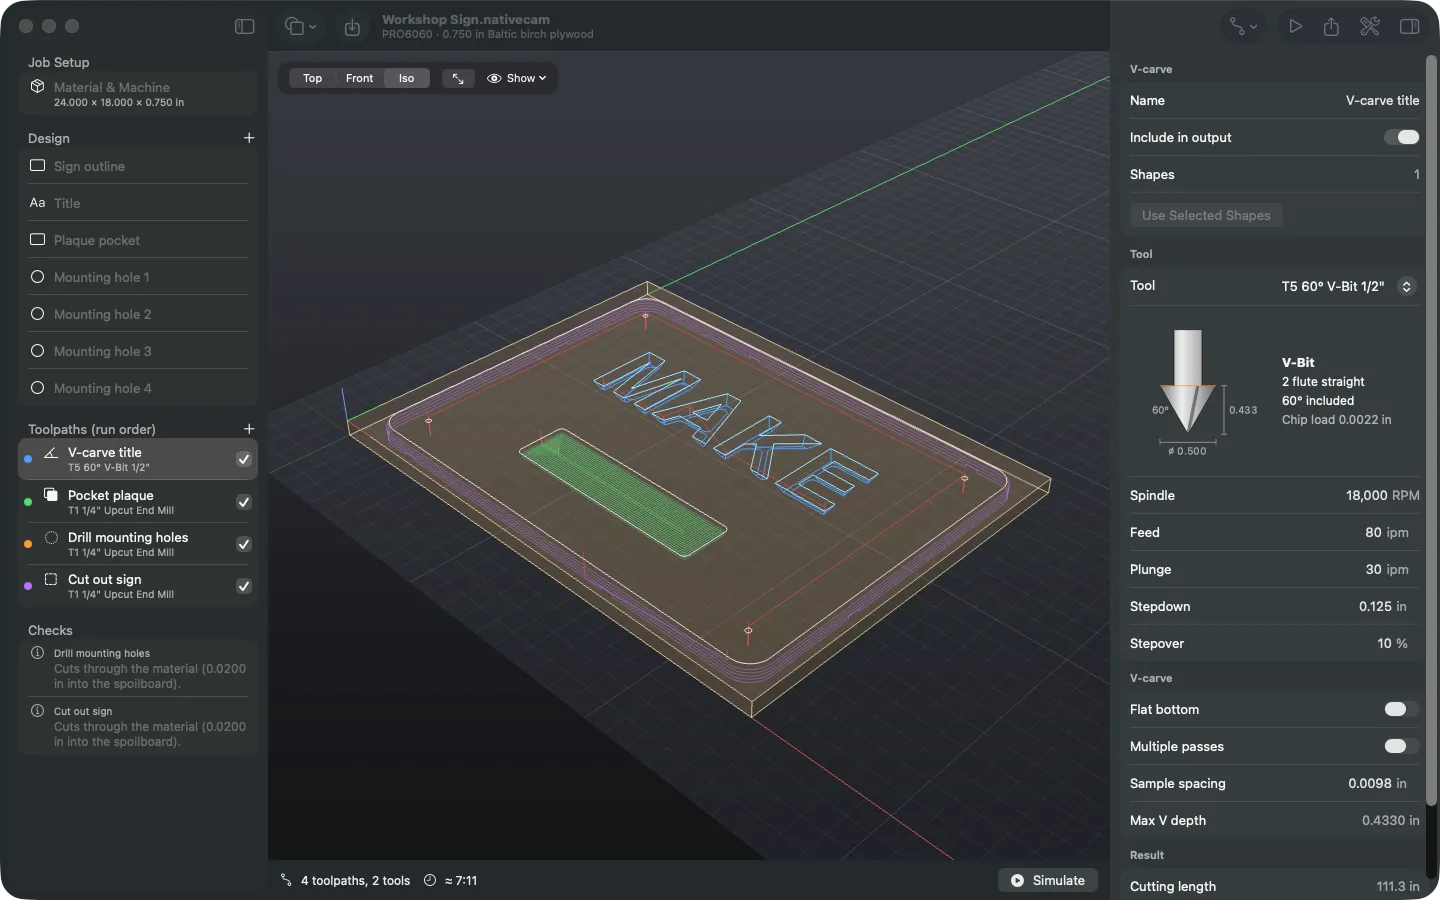
| V-carve | Maximal inscribed circles, a flat-depth cap, an optional flat-area clearing tool, multi-pass. |
| Drill | Peck, chip-break and dwell, written as plain moves. |
| 3D roughing | Layered clearing with an end mill, leaving an allowance for finishing. Layer outlines follow the surface between grid samples instead of stepping cell by cell. |
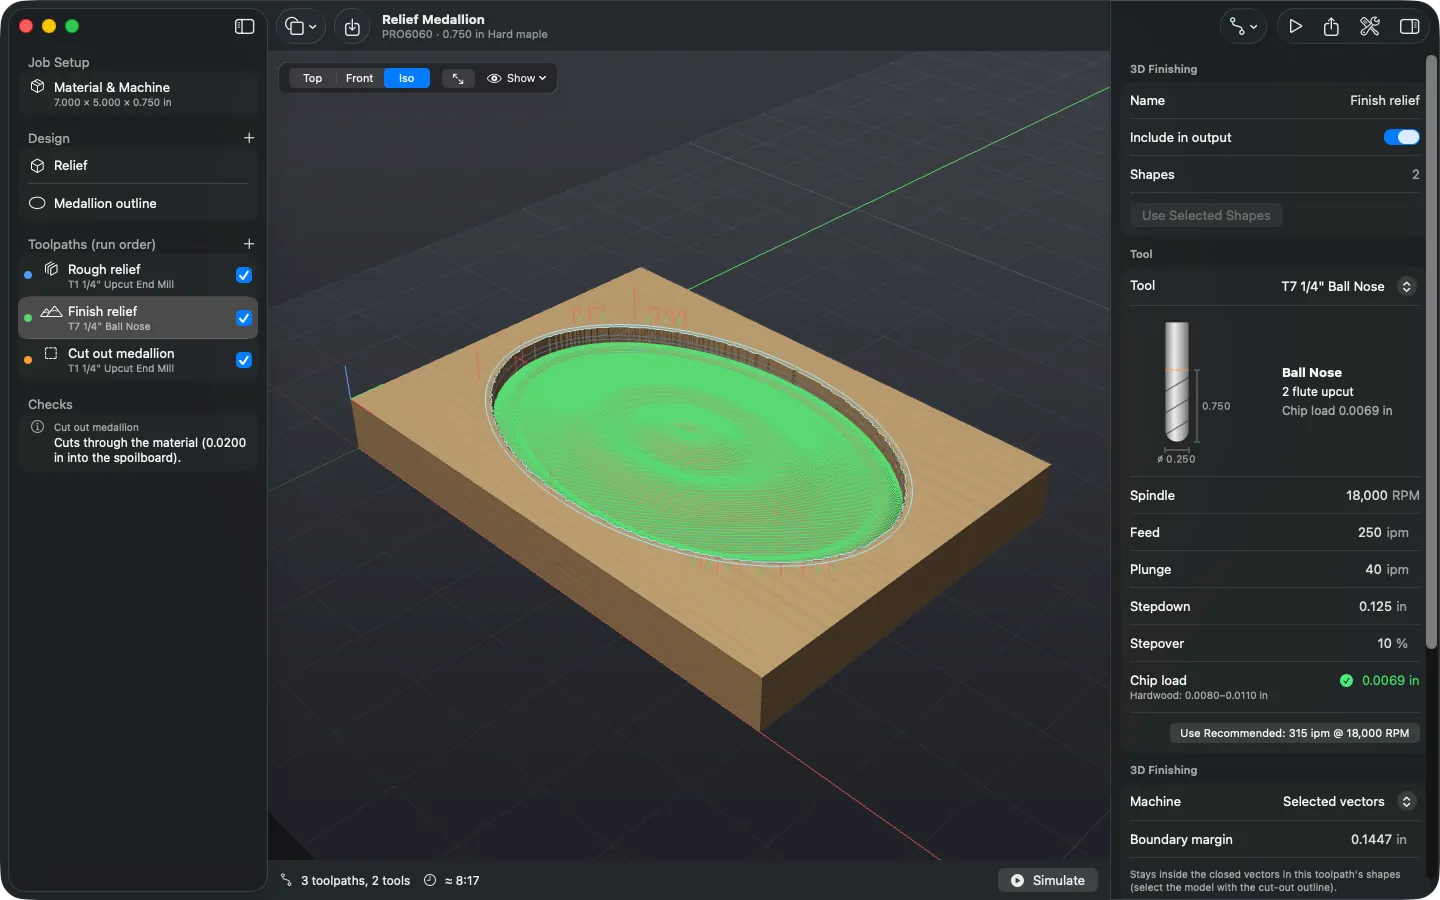
| 3D finishing | Raster passes with an exact triangle drop-cutter for ball and flat bits, so steep walls aren't gouged. Shows the scallop height. |
| Indexed rotary | Profile, pocket and drill toolpaths repeated at a list of angles around a round or square blank (see below). |
Less time in the air. Between cuts the tool rises just above the material that's left plus a safe distance, feeds straight across short stretches already cleared, and rapids down to just above floors this job already cut. Holes, loops and V-carve strokes are ordered by nearest neighbour, then improved by local search. Line segments are re-fitted to arcs, including helical arcs, for controllers that take them.
Job checks as you work. Cuts into the spoilboard or a clamp, depth beyond flute length, toolpaths outside the work area, rapids through material, out-of-range feeds or RPM, chip loads too thin for the material (with a one-click recommended feed), a run order that cuts a part free too early, and two different bits sharing one tool number.
Leads and corner reliefs
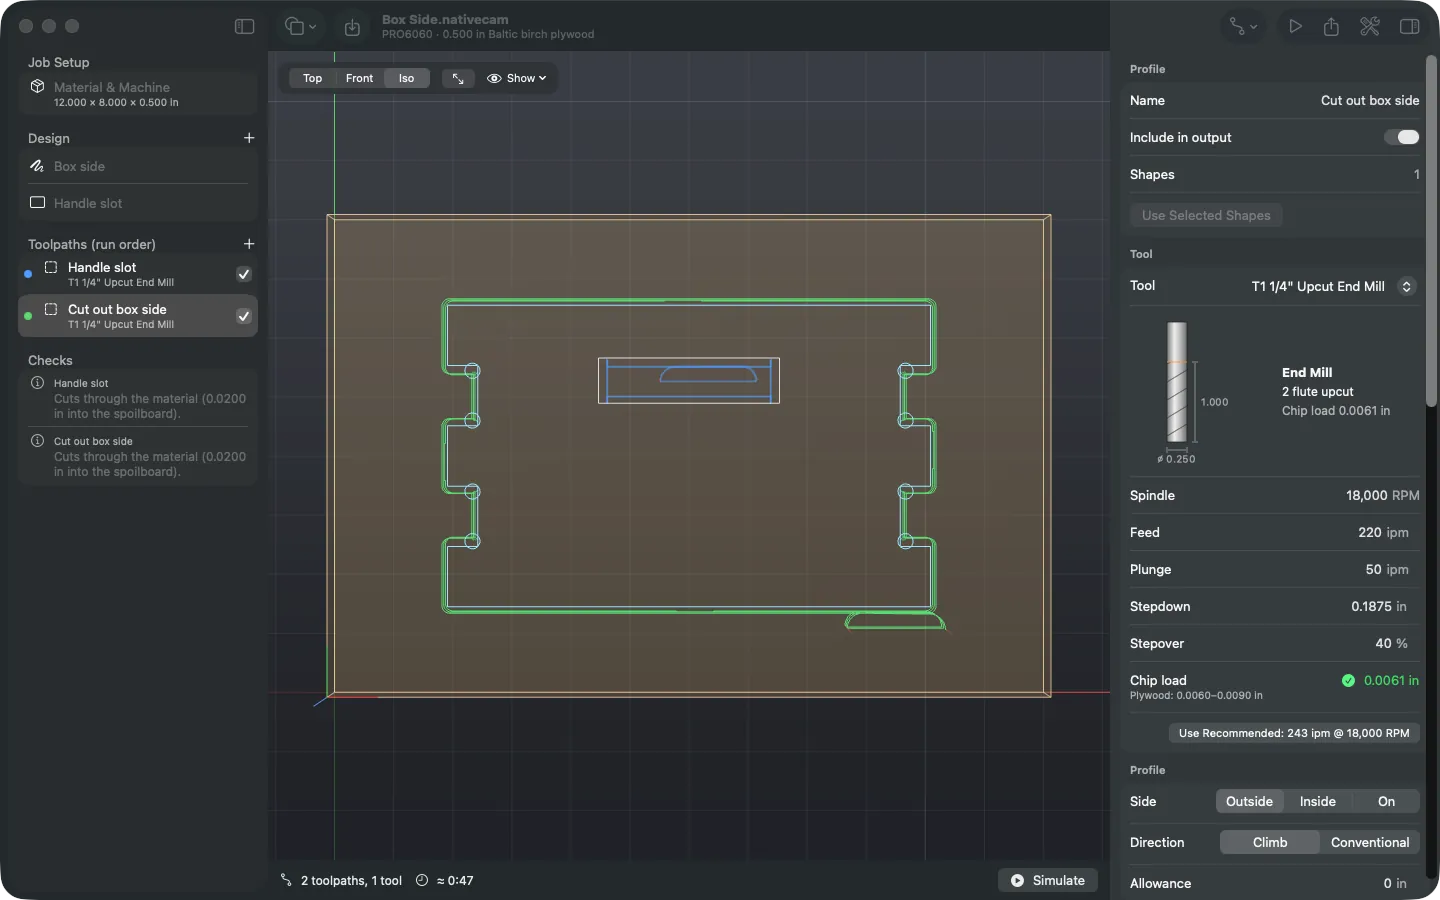
Leads start and end each closed profile loop with a short arc or line in the waste, so the bit never plunges or stops against the finished edge. With a ramp entry the ramp runs down the lead. Leads stay on the waste side, on the material and clear of clamps, and shrink to fit small holes.
Corner reliefs cut just past each inside corner the bit can't reach, so square tenons, tabs and finger joints fit. A dogbone cuts along the corner's bisector; a T-bone cuts along one wall so the notch is only in the other, which suits slots about as wide as the bit.
Each relieved corner is circled on the canvas; click one to switch it between dogbone, T-bone either way, or none. Tutorial →
Indexed rotary (3+1)
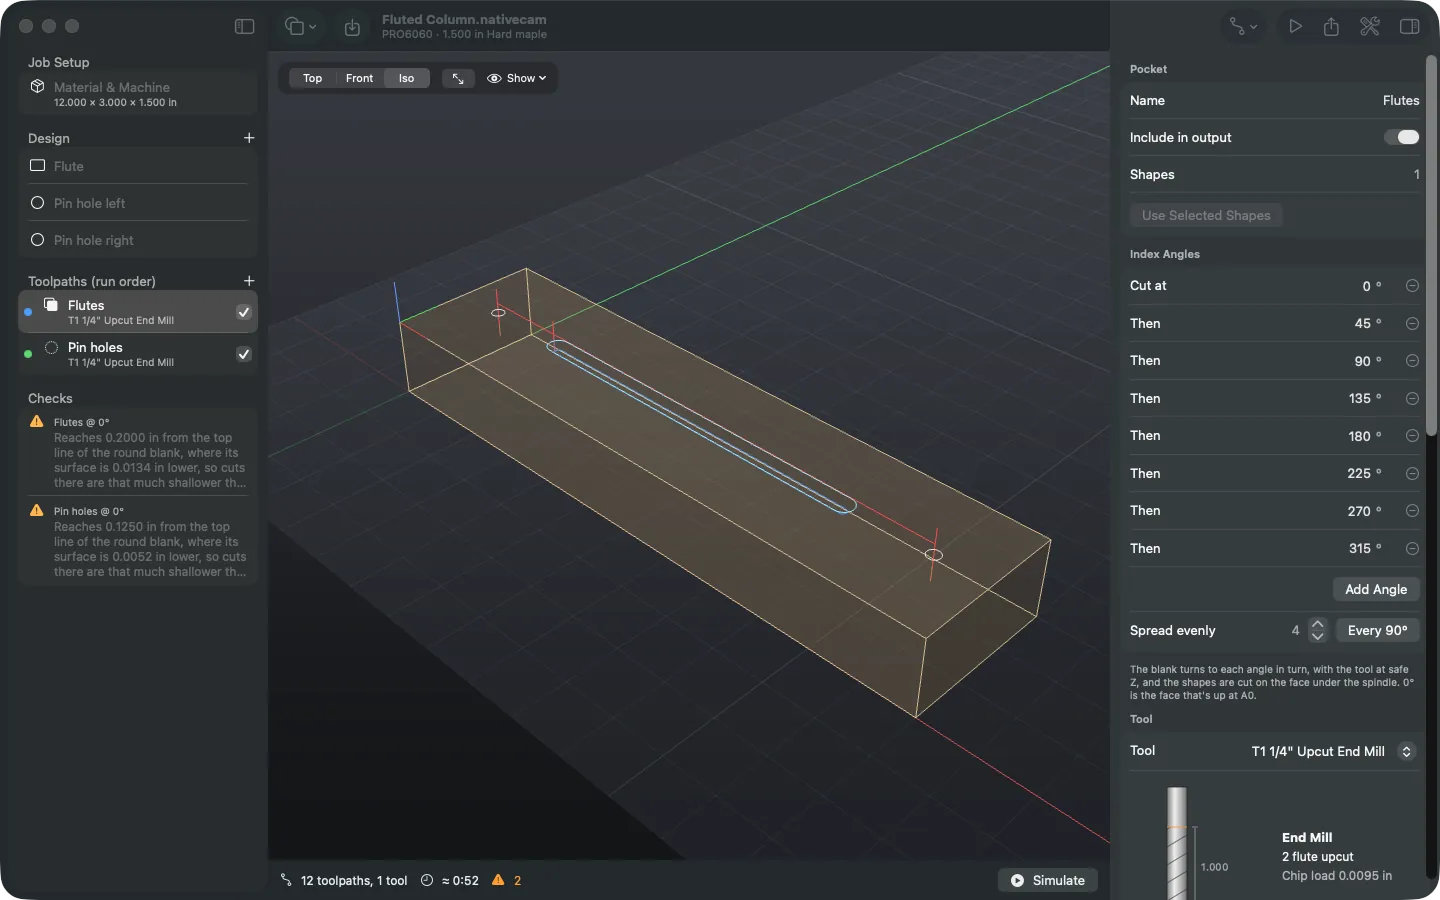
With a rotary axis, the blank turns to a fixed angle, the router cuts the face on top, then the blank turns to the next angle. Profile, pocket and drill toolpaths list the angles they cut at, or Spread evenly fills in a number of faces around the blank.
Round blanks take any angle; square bars take quarter turns. Z zero is on the rotation axis, and the job is checked against your machine's Z travel using the measured centre height. The posts turn the blank with G00 A at safe Z for Avid Mach4, LinuxCNC, grblHAL, Centroid and Buildbotics.
Wrapped (continuous) rotary toolpaths and rotary V-carve or 3D aren't supported yet. Tutorial →
Metal simulation and run times
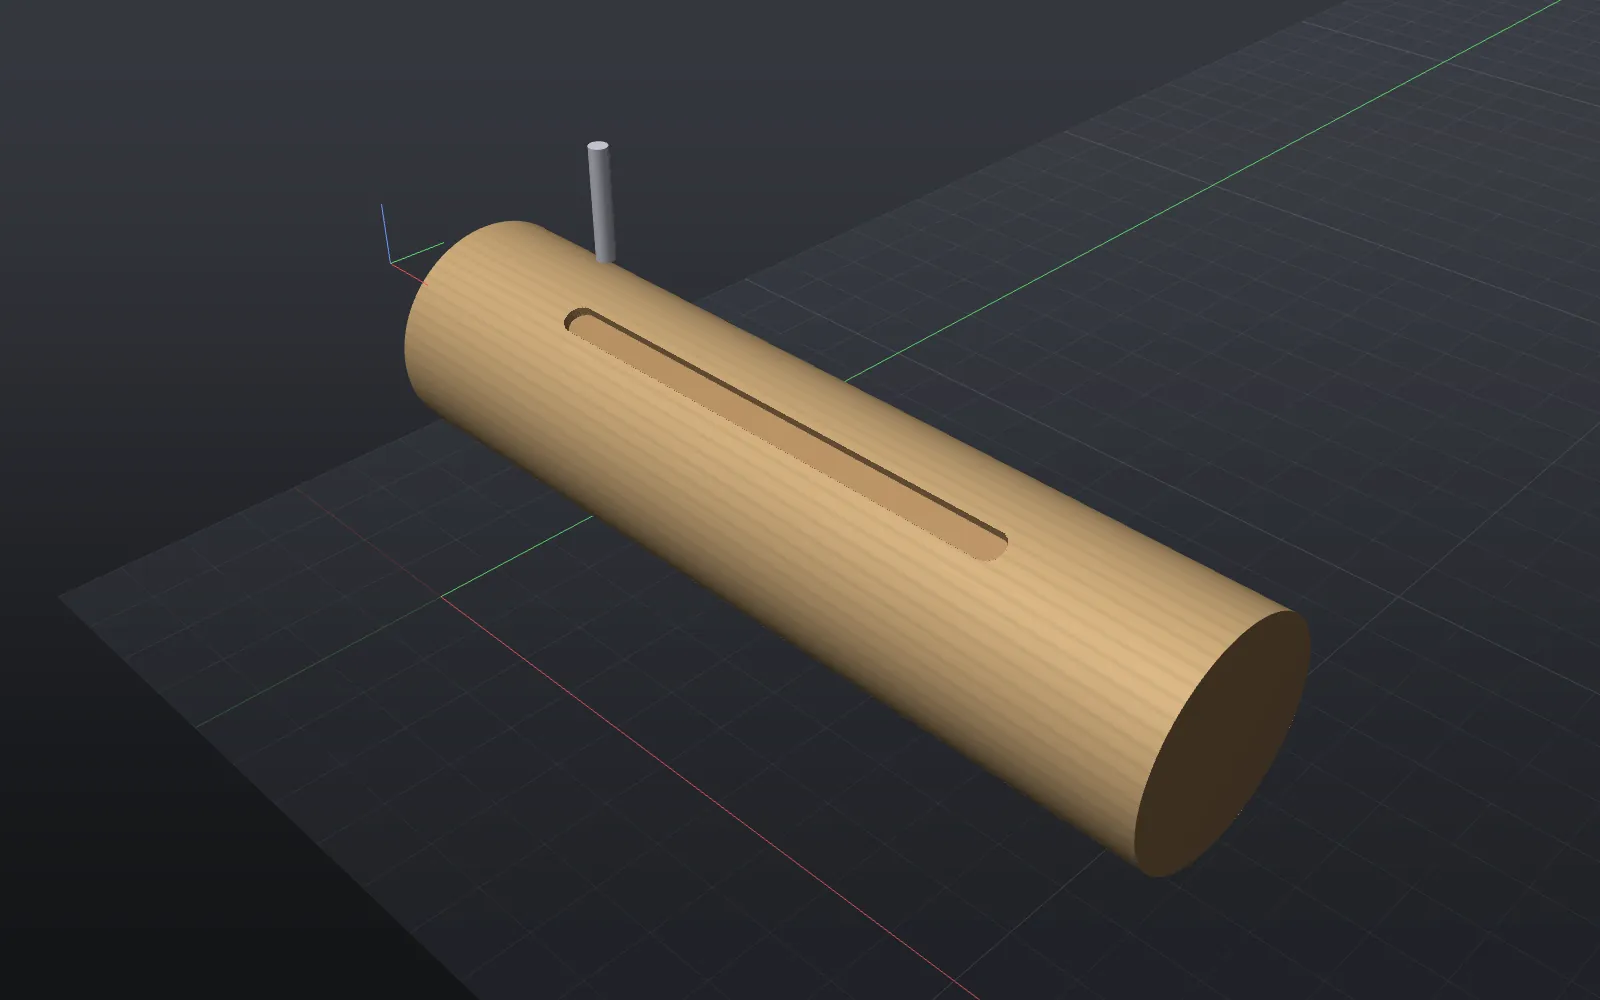
The simulator is a Metal-rendered heightmap carved by the true shape of each bit (flat, ball, bull nose and V), with through-cuts, a tool marker, play, pause, scrub and speed control. It flags rapids through material.
Rotary jobs are carved face by face on the blank itself: it turns to each angle with the tool at safe Z, as the machine will, and slows down for each turn so you can follow it.
Run times come from a model of the controller's own motion planner (per-axis acceleration, corner speeds, look-ahead depth, tool-change and spindle time), not distance divided by feed. They haven't been timed against a real machine yet.
The same simulator opens G-code and ShopBot files from other programs. Tutorial →
Controllers and posts
NativeCAM writes each controller's own dialect, and the export checks hold every file to that controller's rules.
| Controller | Files | Status |
|---|---|---|
| Avid Mach4 | .tap | Run on a real machine |
| Grbl 1.1, grblHAL, FluidNC, Carbide Motion | .nc | From documentation and firmware source |
| LinuxCNC | .ngc | From documentation |
| Masso | .nc | From documentation |
| Centroid CNC12 | .cnc | From Avid's EX posts |
| Buildbotics | .nc | From documentation |
| ShopBot (OpenSBP) | .sbp | From ShopBot's command reference and vendor posts |
| RichAuto DSP | .nc | Conservative; its handling is undocumented |
| Anything else | The post's | With your own Vectric .pp |
For a controller NativeCAM has no post for, Use a Vectric Post… runs the .pp file your machine's maker publishes for VCarve or Aspire as a template, and compares its output with NativeCAM's own post before you use it. The project keeps its own copy; NativeCAM never ships or shares anyone's posts. Controller details → · Vectric post tutorial →
Export checks, air cuts and setup sheets
On export, NativeCAM reads back the file it's about to save and checks it before the save panel appears:
- Against the controller: units, line length, accepted codes, arc radii, feeds, tool numbers, dwell units, spindle on before cutting, a lift to safe Z after each tool change, and no A moves for a controller without a rotary axis.
- Against the toolpaths: every cutting move, arc, feed, dwell, tool and spindle speed is compared with what the toolpaths asked for, which catches post bugs a toolpath simulation can't.
- Against the machine: the whole program, retracts and park included, is measured against the machine's travel and Z travel.
File ▸ Export Air Cut… (⌥⌘E) saves the same program with every Z raised, to run above the material first. File ▸ Export Setup Sheet… saves a printable page for the person at the machine: machine, material and zero, tools in loading order, the run order with tool changes and times, clamps and open checks. Example setup sheet
Machines and controller settings
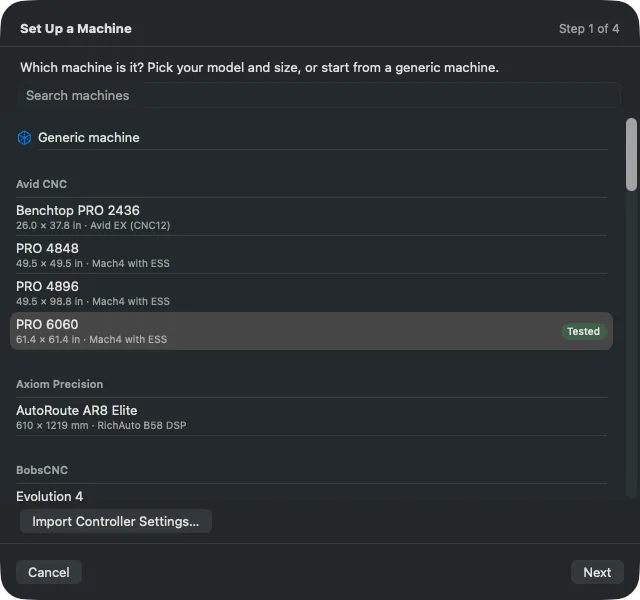
The catalogue holds 37 hobby and prosumer routers from 20 makers, each with the controllers it can run, its travel, spindle, speeds and defaults. Every value has a source: the maker's published specs, the controller settings the maker ships, or a labelled estimate.
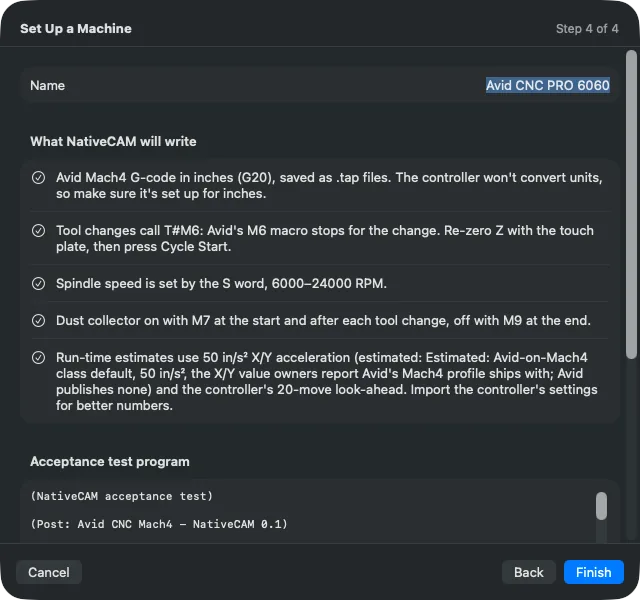
Set Up a Machine… walks through what forum threads show people getting wrong: which controller, which program sends the file, G-code units, tool changes, spindle and dust collector, ending with a plain-language summary and an acceptance test.
Import Controller Settings… reads a Mach4 Machine.ini, Grbl or grblHAL $ output, a LinuxCNC INI, a FluidNC config.yaml or a Fusion 360 .mch for your machine's real speeds, accelerations, travel and spindle range. You choose which values to apply, and each one records where it came from. Tutorial →
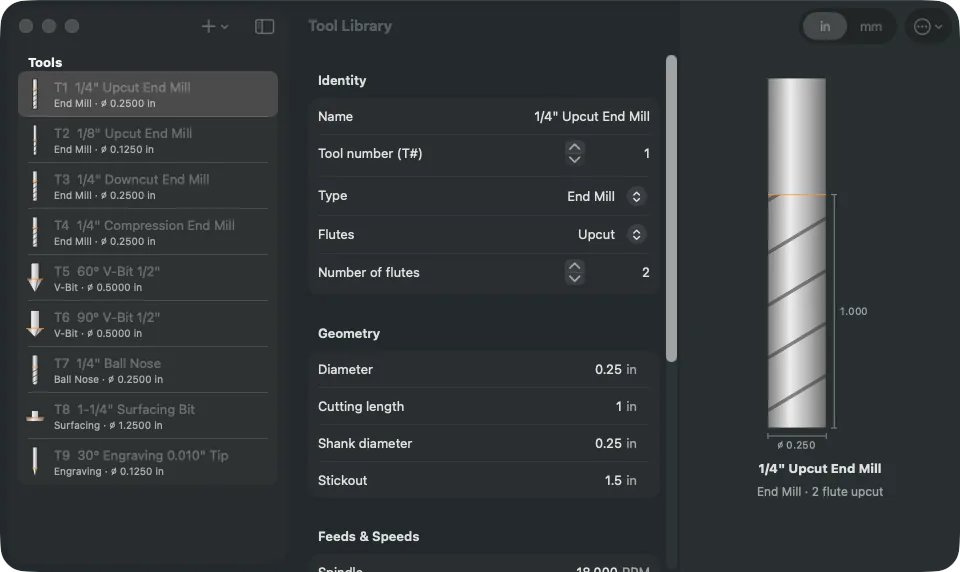
Tool library
Flat, ball, bull nose, V-bit, engraving, surfacing and drill bits with full geometry: flute length, shank, stick-out, flute count and direction, feeds and speeds, and a chip-load calculator checked against chart values for the material. Compression bits get a first pass that clears the upcut length.
Import Tools… reads Fusion 360 .tools and .json libraries, Vectric .vtdb files and NativeCAM's own JSON, listed by the library's folders so you can tick the bits you want. Values a library leaves out are read from the bit's name where possible, otherwise filled conservatively and marked ⚠.
Command line
nativecam-cli runs the same engine without the app, for scripting, CI and checking G-code from other programs:
nativecam-cli demo demo.nativecam                # write the demo sign (demo3d: 3D relief, new: empty project)
nativecam-cli post demo.nativecam -o demo.tap    # generate toolpaths, run checks, write G-code
nativecam-cli post demo.nativecam --air-cut 1 --sheet demo.html   # air cut 1" up, plus a setup sheet
nativecam-cli sim demo.nativecam --png out.png   # simulate and render the result as a heightmap
nativecam-cli sim other-cam-job.tap              # simulate G-code from any CAM program
nativecam-cli tools vendor.vtdb -o tools.json    # convert a Fusion 360 or Vectric tool library
nativecam-cli machine Machine.ini --apply job.nativecam    # read controller limits into a project
nativecam-cli acceptance --controller grbl --units mm      # write the acceptance test for a controller
From the repository, run each as swift run -c release nativecam-cli …. post refuses to write a file that fails its checks unless you pass --force. Full reference →
A real Mac app
Document windows, real menus and keyboard shortcuts, undo, drag-and-drop import, trackpad gestures (pinch to zoom, rotate to spin the view), and Liquid Glass controls on macOS 26. Projects are plain JSON .nativecam documents; older builds refuse to open a format they don't know rather than silently writing the wrong G-code.
| Shortcut | Command | Shortcut | Command |
|---|---|---|---|
| ⌘I | Import | ⌘1 ⌘2 ⌘3 | Top, front, iso view |
| ⌘E | Export G-code | ⌘0 | Zoom to fit |
| ⌥⌘E | Export air cut | ⌥⌘I | Show or hide the inspector |
| ⌘R | Simulate | ⇧⌘T | Tool library |
| ⌘. | Stop simulation | ⌘D | Duplicate |
| ⇧⌘R | Recalculate all toolpaths |